From industrial surface descaling to high-purity contract hygiene chemicals, our lines combine rigorous stability testing, clean chemical engineering, and custom contract manufacturing.
Formulating industrial detergents for the Mumbai Metropolitan Region (MMR) requires advanced surfactant selection, specialized chelating chemistry, and high electrolyte tolerance.
Industrial tap and groundwater across industrial corridors like Thane-Belapur, Taloja, and Tarapur frequently exhibit total dissolved solids (TDS) exceeding 450–800 ppm, saturated with calcium, magnesium, and carbonate ions. Traditional linear alkylbenzene sulfonate (LABS) formulations break down under these conditions, precipitating insoluble metal soaps that choke nozzles and leave chalky scale on parts. Our formulations deploy biodegradable polymeric dispersants and organophosphonate chelators that maintain sequestering thresholds even under fluctuating water parameters.
Operating in proximity to the Arabian Sea exposes heavy machinery, textile autoclaves, and maritime heat exchangers to ambient chloride ions, accelerating galvanic and pitting corrosion. Industrial degreasers and cleaning chemical compounds supplied to Mumbai plants must integrate synergistic corrosion inhibitor packages (such as triazole derivatives and sodium metasilicate pentahydrate) that passivate ferrous and yellow metals throughout the cleaning cycle while cutting heavy mineral oils.
The Maharashtra Pollution Control Board (MPCB) enforces strict COD/BOD and surfactant biodegradation standards for industrial effluent released into common effluent treatment plants (CETPs). Formulations must replace nonylphenol ethoxylates (NPEs) with rapidly readily-biodegradable alkyl polyglucosides (APG) and alcohol ethoxylates. Furthermore, low-temperature foam suppression technology ensures that Clean-in-Place (CIP) rinse cycles do not overflow foam traps or spike biological aeration basin volumes.
Engineered to meet specific mechanical cleaning parameters, soak-tank protocols, and institutional compliance across Maharashtra.
Continuous wet processing, desizing, and scouring of yarn and synthetics require specialized low-foaming scouring agents with thermal stability up to 90°C.
Heavy fuel oil, bitumens, and grease descaling inside marine cargo tanks, shipboard bilges, and refinery transport pipeworks require high-flashpoint solvent degreasers.
Validated CIP and SIP detergent formulations that yield zero analytical residues on 316L stainless steel vessels, verified via Total Organic Carbon (TOC) analysis.
Multi-stage ultrasonic cleaning and spray washer detergents designed to strip quenching oils, swarf, and metal filings without staining aluminum alloys.
Combining American R&D rigor, lean ingredient philosophy, and audited high-volume filling capabilities designed to lower procurement friction.
We eliminate filler salts and superfluous stabilizing additives, formulating with the purest active components. This approach reduces overall batch weight, cuts per-liter shipping logistics costs to Mumbai sea entry points, and mitigates batch-to-batch variation.
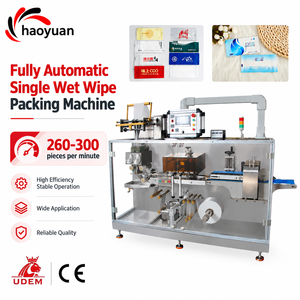
Scalable output capacity powered by automated high-speed machinery capable of packaging 65,000 tubes and over 150,000 flex units every day. We support institutional concentrates in 5-gallon carboys, 55-gallon drums, and 1,000-liter IBC containers.
Every lot is blended under comprehensive Current Good Manufacturing Practice (cGMP) compliance, complete with detailed Certificates of Analysis (COA), full traceability of raw materials, and documented SMETA ethical trading accountability.
 cGMP Certified
 USDA Standard
 Eco-Certified
 Soil Association
 SMETA Audited
 EPA Compliant
Essential details regarding cross-border chemical logistics, import tariffs, batch validation, and shelf-life stability.
All international consignments are supplied under explicit Harmonized System (HS) codes (such as Chapter 34 for surface-active preparations and cleaning compounds), accompanied by GHS-compliant Safety Data Sheets (SDS), detailed non-DG declarations when applicable, and verified Certificates of Analysis (COA) to prevent customs delays at Nhava Sheva.
Yes. Storage conditions across Bhiwandi and Panvel warehouses routinely face ambient temperatures exceeding 38°C and humidity over 85%. Our R&D chemists run accelerated stability and freeze-thaw cycles to prevent emulsion breakdown, phase separation, or polymer degradation during long-term seasonal storage.
We accommodate both trial pilot runs for commercial validation and full-container replenishment programs. Minimum lot sizes depend on the viscosity, packaging format (5-gallon carboys vs. automated pouch filling), and specific active ingredient decks. Contact our technical team for custom project scoping.
Yes. For cleanroom and pharmaceutical processing facilities in Thane and Raigad, we deliver complete rinse-verification data packets, TOC determination methodologies, and electrical conductivity profiling to streamline your facility's validation under USFDA or local regulatory audits.
Speak with our formulation chemists and export specialists to configure chemical solutions optimized for your specific machinery, water hardness parameters, and regulatory requirements.