Explore our CE-certified vacuum homogenizing emulsifiers, complete mixing lines, and high-barrier packaging systems optimized for personal care manufacturing.
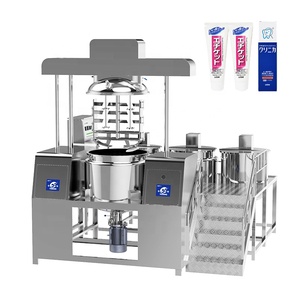
A rigorous examination of European Conformity (CE) compliance, mechanical shear dynamics, and cGMP validation protocols essential for modern cosmetic contract packaging and equipment sourcing.
Procuring cosmetic processing equipment carrying authentic CE Certification mandates strict compliance with three non-negotiable European Union Directives. Equipment designated for high-viscosity body lotions, emulsions, and rich body butter blends must adhere to integrated electrical, mechanical, and operational safety criteria:
Under regulation (EC) No 1223/2009 (EU Cosmetics Regulation), equipment cleanliness directly impacts the final Cosmetic Product Safety Report (CPSR). Machinery surfaces in contact with raw liquid phases must be engineered from AISI 316L electro-polished stainless steel with internal surface roughness rating of Ra ≤ 0.4 μm to eliminate bacterial biofilm accumulation.
CE-certified machinery must seamlessly integrate into cGMP facility validation schemes:
Comparing vacuum homogenizers, high-shear mixers, and automated packaging lines across vital manufacturing metrics.
| Equipment Category | Batch / Daily Capacity | Rotor-Stator Shear Speed | Vacuum Operating Pressure | Thermal Control Jacket | Primary Industrial Application |
|---|---|---|---|---|---|
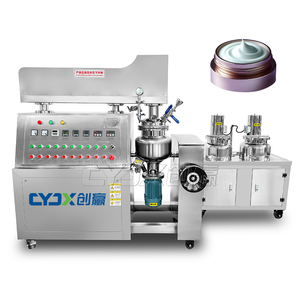
| 5L R&D Pilot Vacuum Emulsifier | 1 L – 5 L / Batch | 0 – 3,600 RPM (Variable) | -0.09 MPa Vacuum | Electric / Hot Water (-0.5 bar) | Formulation R&D, Pilot Scaling & Small Batch Creams |
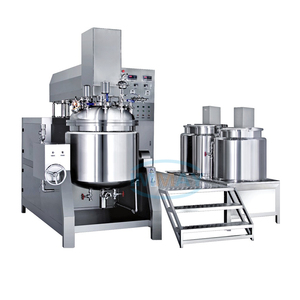
| 200L High-Shear Body Lotion Homogenizer | 50 L – 200 L / Batch | 0 – 2,800 RPM (Bottom/Top) | -0.092 MPa Deaeration | Steam / Thermal Oil Jacket | Medium Scale Commercial Lotions & Serums |
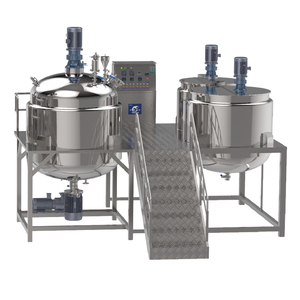
| Industrial Cosmetic Production Line | 500 L – 5,000 L / Batch | Dual Anchor 0-65 RPM + Shear | Continuous Vacuum System | Isolated Dual Heat/Cool Circuits | Mass Market Body Moisturizers & Heavy Ointments |
| High-Speed Tube Filling & Sealing Line | Up to 65,000 Tubes / Day | Piston / Servo Volumetric | Nitrogen Purging Option | Hot Air Inner Seal Unit | PBL / ABL Barrier Laminate Tube Packaging |
| Flexible Unit Filling Machinery | Up to 150,000 Units / Day | Multi-Head Rotary Peristaltic | Inline Vacuum Capping | Ambient to Warm Fill System | Bottles, Jars, Flex-Pouches up to 5 Gallons |
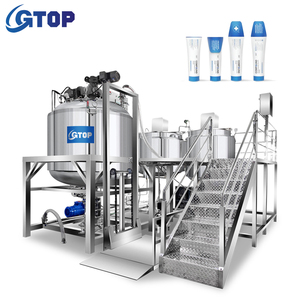
Body lotions rely on stable Oil-in-Water (O/W) or Water-in-Oil (W/O) structures. CE-certified high-shear vacuum emulsifiers utilize dual-action counter-rotating wall scrapers combined with a precision rotor-stator generator. Scrapers prevent product scorching against jacket walls while forcing bulk liquid into the central high-shear zone.
At shear rates exceeding 100,000 s¹, oil droplets are broken down into sub-micron particles (0.2 to 2 microns). Micro-emulsification prevents droplet coalescence, sedimentation, and phase separation under extreme thermal stress tests (45°C freeze-thaw cycles).
Entrapped air bubbles inside rich skin creams cause product oxidation, rancidity of natural lipids, and weight inaccuracy during tube filling. Integrated vacuum degassing (-0.09 MPa to -0.095 MPa) strips micro-aeration from the matrix prior to cooling.
Deaeration produces a glossy, high-end surface finish, extends shelf life, and ensures exact volumetric dosing when filling automated squeeze tubes or airless pump containers.
Key shift analysis for sourcing directors, brand owners, and procurement specialists managing global supply chains and clean beauty transitions.
Modern consumers demand short, transparent ingredient lists. Contract manufacturing requires precise blending of active botanicals, hyaluronic acid complexes, and bio-fermented lipids without heavy chemical stabilizers or synthetic thickeners.
To reduce thermal degradation of delicate bio-actives and meet corporate ESG targets, manufacturers are transitioning to cold-process polymeric emulsifiers, cutting production thermal cycles by up to 60%.
Procurement teams are prioritizing PBL (Plastic Barrier Laminate) squeeze tubes with flip-top lids, PCR (Post-Consumer Recycled) resin blends, and mono-material recyclable pump structures to meet European green packaging directives.
Combining US-based manufacturing excellence with global compliance, custom R&D expertise, and massive scale flexibility under one accountable roof.
Reforma Group operates out of state-of-the-art facilities in Southfield, Michigan. By keeping R&D, custom blending, vacuum emulsification, inline filling, packaging, and distribution under domestic oversight, we eliminate international transit bottlenecks and guarantee strict adherence to federal safety benchmarks.
Our infrastructure accommodates flexible unit fills up to 5-gallon containers and high-speed filling capacities exceeding 65,000 tubes per day and 150,000 flex units per day. Whether you are scaling an emerging clean beauty DTC lineup or sustaining enterprise retail distribution, our operations maintain uniform quality across every SKU.
Our quality control systems align with international cosmetic and pharmaceutical audit standards:
 cGMP
 USDA
 COSMOS
 Soil Assoc.
 SMETA
 FDA Registered
Comprehensive answers regarding machine engineering, contract manufacturing, compliance dossiers, and scale-up timelines.
Every CE-marked production system includes an exhaustive Technical File comprising the official Declaration of Conformity (DoC), Machinery Directive 2006/42/EC risk assessments, LVD electrical safety test reports, EMC emissions certificates, material pressure vessel certificates (PED 2014/68/EU where applicable), 3.1 stainless steel material traceability certificates (EN 10204), and full IQ/OQ/PQ validation templates.
Conventional open mixing tanks introduce ambient air into liquid creams, causing micro-foaming, bulk density inconsistency, oxidic degradation of fragile natural botanical actives, and high microbial contamination risks. Vacuum emulsifiers operate under negative pressure (-0.09 MPa), stripping trapped air, accelerating phase emulsification, reducing droplet size to 0.2-2 microns, and delivering a luxurious, high-gloss texture with superior long-term shelf stability.
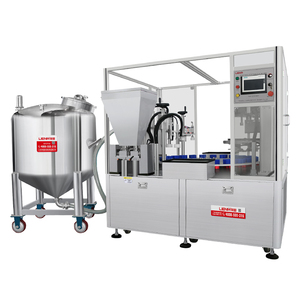
Our automated production facilities feature dedicated high-speed filling lines capable of processing up to 65,000 tubes per day (PBL, ABL, or aluminum squeeze tubes) and up to 150,000 flexible units per day across various bottles, jars, and pumps ranging from travel-size containers up to 5-gallon bulk pails.
Yes. CE-certified multi-function vacuum mixers feature dual variable frequency drives (VFD) that allow independent control of the central anchor scraper (10-65 RPM) and bottom/top high-shear homogenizer (300-3600 RPM). This flexibility enables seamless processing of low-viscosity moisturizing milks (1,000 cP) up to high-viscosity body butter ointments exceeding 100,000 cP without motor strain or thermal hot-spots.
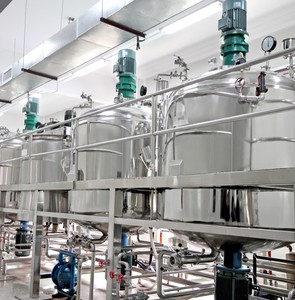
Our industrial mixing vessels are equipped with 360-degree rotating sanitary spray balls connected to automated CIP/SIP skids. The system circulates heated water, detergent wash, and purified water rinses through sanitary diaphragm valves and electro-polished piping, achieving total batch residue elimination and zero cross-contamination between different brand SKUs.
Reforma Group's in-house R&D chemists and formulation engineers offer end-to-end support—from initial concept formulation using clean, minimal ingredients to pilot bench trials (5L pilot mixers) and seamless commercial scale-up (200L to 5,000L production runs). We assist with stability testing, preservative efficacy testing (PET), microbial challenge tests, and packaging compatibility evaluations.
Connect with our engineering and procurement team to request comprehensive machinery specifications, custom formulation quotes, or product catalog documentation.