Discover high-performance private label cleaning formulas, industrial process lines, and customized commercial care chemistries engineered to global compliance marks.
The global market for institutional and industrial (I&I) detergents demands an unprecedented level of formulation rigor, environmental compliance, and high-shear synthesis accuracy. Selecting an industrial detergent formulation factory is no longer a matter of comparing unit spot pricing; it is a critical calculation of surfactant kinetic stability, environmental stewardship, and supply chain continuity. Unregulated contract compounders that deliver subpar, heavily diluted surfactants with inconsistent batch viscosity jeopardize enterprise operations, create substantial liability, and fail stringent EPA and OSHA workplace regulations.
Modern enterprise procurement directors prioritize manufacturing partners operating under validated cGMP manufacturing frameworks and certified quality control regimes. A premier formulation plant must combine comprehensive in-house wet chemistry R&D with multi-metric mechanical throughput—spanning vacuum emulsification blending, precision chemical filling, and integrated global supply chain distribution.
By engineering custom formulations with the fewest, purest active ingredients necessary, manufacturers eliminate fillers, reduce unwanted volatile organic compounds (VOCs), and deliver hyper-concentrated products that drastically reduce shipping freight and carbon footprints.
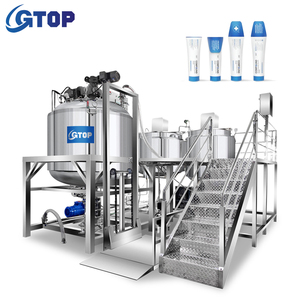
Advanced synthesis involving high-shear vacuum homogenizers guarantees absolute dispersion of non-ionic, anionic, and amphoteric builders, preventing phase separation across extreme hot and cold storage cycles encountered in logistics corridors.
Top-tier manufacturing facilities formulate in lockstep with EPA Safer Choice, OSHA Hazard Communication standards, and regional aquatic toxicity regulations, supplying pre-cleared Safety Data Sheets (SDS) and global documentation on demand.
As regulatory frameworks tighten worldwide, procurement teams must align their chemical acquisition schedules with macro trends reshaping commercial detergents over the next decade. Industry shifts indicate that legacy phosphate-heavy formulas and petroleum-derived solvent degreasers are being rapidly phased out in favor of green chelation, biosurfactants, and high-density liquid concentrates.
Transition from petroleum-based ethoxylated surfactants to sophorolipids and rhamnolipids. These bio-based cleansers offer low ecotoxicity profiles, superior surface-tension reduction, and exceptional biodegradability without compromising caustic grease stripping.
Enterprise logistics models favor closed-loop dilutable super-concentrates in intermediate bulk containers (IBCs) and drum flex systems. Reducing water transit volume delivers up to 60% savings on long-haul transport and mitigates plastic resin consumption.
Global brands are abandoning disjointed multi-vendor models. Leading suppliers provide vertically integrated capabilities: chemical synthesis, inline viscosity control, custom blow molding, label printing, and intermodal domestic and overseas fulfillment under one roof.
Operating from Southfield, Michigan, Reforma Group embodies engineering excellence in custom formulating, high-throughput filling, and international brand deployment. With dedicated facilities manufacturing 100% in the United States, we offer corporate clients, international distributors, and commercial labels an end-to-end framework shielded from global supply interruptions and regulatory inconsistencies.
Our formulation engineering team delivers high-yield processing lines capable of packaging up to 65,000 tubes per day and 150,000 flex units per day, scaling flexibly up to 5-gallon bulk units. We bridge pure laboratory research with industrial mass-scale compounding, upholding strict cruelty-free protocols across personal, pet, and institutional care programs.
 cGMP Certified Facility
 EPA Regulatory Cleared
 SMETA Ethical Audit
 FDA Compliant Process
Essential operational, formulation, and compliance clarifications for technical buyers and procurement officers.
Procurement directors must verify manufacturing execution capabilities across several vital metrics: cGMP batch-traceability protocols, on-site high-shear vacuum homogenization systems, dynamic viscosity stabilization (Brookfield standards), flash-point verification for solvent cleaners, and comprehensive microbiological testing. Furthermore, a qualified facility should provide turnkey GHS-compliant Safety Data Sheets (SDS), certificates of analysis (CoA) per lot, and EPA environmental impact documentation.
Our core R&D philosophy focuses on "minimal-ingredient engineering." Rather than loading formulas with inactive stabilizers, thickeners, and unnecessary chemical ballast, we utilize high-purity surfactants and concentrated active builders that achieve target cleaning kinetics with fewer raw compounds. This lean chemistry design reduces raw material expenditures, simplifies regulatory clearance, minimizes supply chain vulnerabilities, and delivers superior profit margins across mass retail, janitorial, and private enterprise distributions.
Reforma Group provides filling infrastructure covering everything from small consumer-facing trial containers and 65,000 tubes/day lines to large institutional and industrial containers up to 5-gallon pails and flex dispensing systems. Custom bottling, labeling, and direct-fill industrial packaging are managed in-line within our domestic Michigan facilities to guarantee seamless container compatibility and zero chemical stress-cracking.
Yes. Our in-house chemical engineers and custom blending teams formulate zero-residue, low-foaming, non-corrosive, and non-ionic formulations specifically designed for specialized substrate washing, electronic component defluxing, precision tooling, and food processing plant CIP (clean-in-place) systems. Formulation parameters such as pH, conductivity, and rinse-off speed are calibrated to the exact operating requirements of your end clients.
Once client artwork and technical formulation specifications are finalized, standard pilot batching and stability approvals are completed rapidly. Production filling operates across automated lines running up to 150,000 units daily. Our integrated supply chain management team coordinates domestic freight, bonded warehousing, customs documentation, and international shipping logistics, ensuring that commercial orders arrive promptly at target seaports and distribution centers worldwide.
Partner with an American chemical synthesis leader. Contact our engineering team today to review custom detergent formulations, obtain product technical sheets, or schedule a pilot production run.