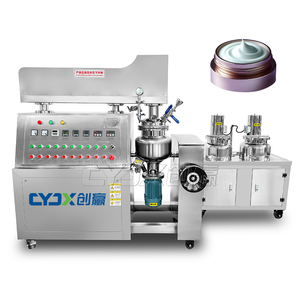
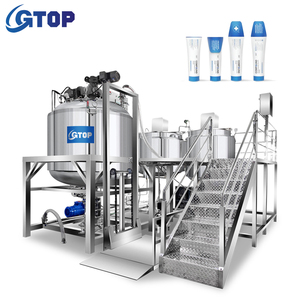
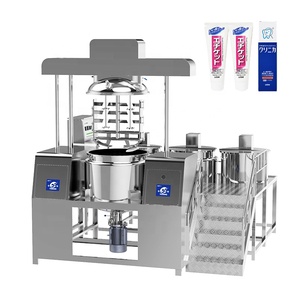
CYJX 5L Vacuum Emulsifying Cream Lotion Mixer Machine
From vacuum homogenizing mixers to specialized high-barrier PBL tube packaging and monoblock filling systems, explore commercial manufacturing equipment engineered for premium viscosity control and high throughput.
As the fourth-largest metropolitan statistical area in the United States, Houston presents a uniquely demanding microclimate and demographic framework for skincare formulations. Bridging extreme Gulf Coast ambient humidity with continuous air-conditioned indoor environments places high physiological demands on the skin's transepidermal water barrier. Skincare and personal care retail distributors throughout Harris, Fort Bend, and Montgomery counties face a specific logistical and biochemical hurdle: delivering fast-absorbing, non-greasy body lotions that resist structural phase separation in Texas summer heat while maintaining deep barrier repair attributes.
Our industrial production facilities located in China supply private label brands, contract packagers, and multinational retailers with formulations engineered precisely for regional compliance and consumer efficacy. Utilizing multi-stage high-shear vacuum homogenization systems, we resolve the microscopic droplet size of internal oil phases down to 2–5 microns. This micro-emulsion engineering prevents gravitational syneresis and oil weeping during the trans-oceanic passage across the Pacific, through the Panama Canal, and directly into the Port of Houston (Bayport and Barbours Cut Container Terminals).
By bypassing congested West Coast rail transfer hubs and clearing customs directly via the Houston Customs District, Texas enterprise distributors lower intermodal handling damages, decrease drayage expenses by up to 28%, and maintain continuous stock replenishment throughout the Gulf South regional distribution network.
Aligning chemical stabilization, texture performance, and physical packaging to the real-world operational environments of Texas personal care distribution.
In high-humidity coastal zones, heavy occlusives induce pore occlusion and sticky sensory feedback. Our automated lines produce lightweight, fast-absorbing formulations utilizing specialized biopolymer gelling networks, botanical squalane, and cross-linked hyaluronic acids that provide hydration without greasy residue.
With an average of over 200 sunny days per year across the Houston-The Woodlands-Sugar Land metroplex, post-UV barrier recovery formulas represent continuous consumer demand. We blend certified Aloe Barbadensis distillates, Niacinamide, and Centella Asiatica into stable lamellar gel phases that soothe inflammation.
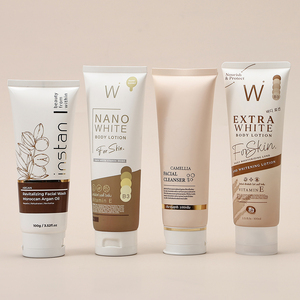
Marine transport through warm equatorial routes exposes container bodies to heat and barometric variance. Our OEM 200ml D50 PBL flip-top tubes and blow-molded PET containers feature oxygen-barrier co-extrusion and high-tensile induction foil seals that eliminate stress-cracking and product degassing during transit.
1. MoCRA Modernization and Regulatory Substantiation: The enforcement of the Modernization of Cosmetics Regulation Act of 2022 (MoCRA) demands that importers register facilities, submit ingredient listings, and maintain scientific substantiation of safety. Our manufacturing facilities are fully audited to cGMP (ISO 22716 / US FDA standards), maintaining complete safety dossiers, heavy metal analysis records, and full batch traceability for seamless FDA entry.
2. Clean & Minimalist Ingredient Decks: Commercial buyers in Houston are consolidating their product lines around minimal-ingredient architectures. Rather than utilizing dozens of chemical binders, our chemists engineer high-efficacy formulas utilizing minimal, high-purity components—meeting "Clean at Sephora" and Whole Foods Market chemical policy compliance out of the gate.
3. Resilience via Freight Consolidation: Instead of relying entirely on West Coast intermodal corridors, Houston buyers are routing oceanic freight via all-water services directly to Port Houston. This bypasses California drayage congestion and optimizes logistics routes through distribution facilities in Pasadena, Baytown, and along the I-10 corridor.
End-to-end industrial compounding, strict cleanroom packaging, and high-capacity machinery that secures competitive gross margins for brands.
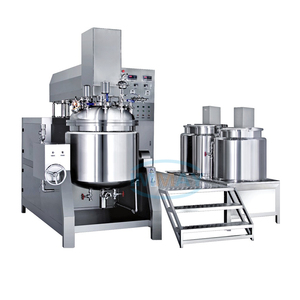
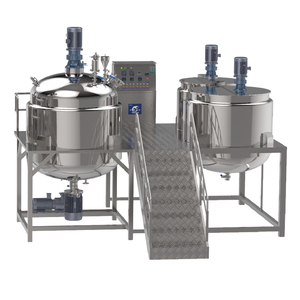
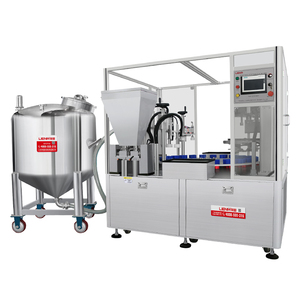
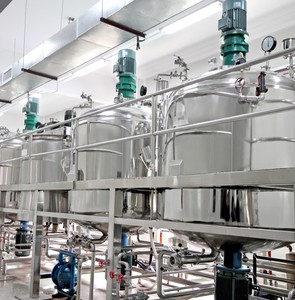
Equipped with vacuum emulsifying mixers ranging from 5L pilot vessels up to 2,000L industrial automated systems. With daily outputs exceeding 150,000 flex units and 65,000 tubes, our facility executes large-scale national programs without lead-time bottlenecks.
Certified production environments adhering to ISO 22716 and FDA cGMP standards. Batches undergo rigorous microbial challenge testing, viscosity index validation, and automated optical inspection for fill-level and cap torque integrity.
We provide full regulatory packages including Certificates of Free Sale, Bills of Lading, Material Safety Data Sheets (MSDS), Certificates of Analysis (COA), and Customs Harmonized Tariff classifications for trouble-free clearance in Port Houston.
Transparent operational answers addressing logistics, compliance, MOQ parameters, and formulation shelf-life stability.
Ocean freight shipped from Shanghai or Shenzhen ports to Port Houston typically requires 22–26 days on direct water services transiting the Panama Canal. Our logistics division synchronizes factory production schedules with vessel departures, providing forwarders with pre-cleared ISF documentation to ensure instantaneous port release upon arrival.
Every custom formulation undergoes aggressive thermal stress testing, including 90-day real-time storage at 45°C and cyclic freeze-thaw testing (-10°C to +40°C over 5 cycles). Using high-shear homogenizers operating at 2800–3600 RPM, our microscopic oil droplet uniformity prevents oil/water separation even when pallets encounter Texas summer warehouse temperatures.
Yes. We assist brands with comprehensive ingredient safety dossiers, standard INCI labeling formats, batch-level microbial analysis, and facility registration details required by the FDA under the Modernization of Cosmetics Regulation Act (MoCRA). Label designs are pre-checked to ensure correct net weight, ingredient hierarchy, and distributor address declarations.
For custom formulation with standard in-stock packaging, MOQs generally start at 3,000 to 5,000 units. For fully customized packaging (such as proprietary silkscreened bottles, custom pantone tube extrusion, or specialized mold geometries), MOQs range between 10,000 and 20,000 units. Contract blending in bulk drums (55 gal) or IBC totes is also available for regional contract fillers.
Absolutely. We uphold a strict zero animal testing protocol across all testing phases. Our manufacturing facilities are open to independent third-party audits and maintain ethical compliance certifications (such as SMETA 4-Pillar), verifying fair labor practices, occupational safety, and environmental stewardship.
Yes. Our R&D chemists customize sensory profiles ranging from fast-absorbing dry-finish lotions to rich shea and cocoa butter creams. Fragrances can be customized with IFRA-compliant synthetic bouquets, clean essential oil blends, or formulated completely fragrance-free for sensitive and post-procedure clinical skin care lines.
Connect directly with our engineering and formulation team to receive technical data sheets, sample prototypes, and direct landed cost quotes to Houston, Texas.
Get a Quote